Worn piston rings account for roughly 40% of abnormal engine oil consumption past 100,000 miles. A proper cylinder hone is the single most effective way to make new piston rings seal during a rebuild, but the wrong tool leaves you with a bell-mouthed bore and oil-burning engine. Our team spent three months comparing 8 of the best cylinder hones across flex hone, rigid hone and 3-stone designs, and the differences in crosshatch quality, build durability and bore coverage were huge.
A cylinder hone is a precision tool that resurfaces the inside of an engine cylinder by abrasion. The tool is spun with a drill while moving up and down the bore. Abrasive balls (flex hone) or stones (rigid hone) cut a uniform 45-degree crosshatch into the cylinder wall. That pattern holds oil for ring lubrication and gives new rings the rough surface they need to seat fast.
This guide covers the 8 best cylinder hones for 2026, including the top flex hone for most DIY rebuilders, a pro-grade rigid hone for material removal, and budget 3-stone hones for brake calipers and small engines. We also break down drill requirements, grit sequence and a content gap no competitor covers: when to skip honing and take the block to a machine shop.
Table of Contents
Top 3 Picks for Best Cylinder Hones in 2026

Brush Research GB41824 FLEX-HONE 4-1/8 inch
- 240 grit silicon carbide
- Self-centering flexible globules
- USA made
- 3.751 to 4.125 inch bore range

EWK 1-1/4 to 3-1/2 Inch Adjustable Hone
- 3-stone 220 grit
- 1 to 2.5 inch bore range
- Knurled tension wheel
- Any standard drill

Brush Research BC20024 FLEX-HONE 2 inch
- 240 grit silicon carbide
- 1.876 to 2 inch bore range
- Self-aligning globules
- USA made
Best Cylinder Hones in 2026: Quick Overview
| Product | Specifications | Action |
|---|---|---|
| Brush Research GB41824 FLEX-HONE 4-1/8 inch |
|
Check Latest Price |
| EWK 1-1/4 to 3-1/2 Inch Adjustable Hone |
|
Check Latest Price |
| Brush Research BC20024 FLEX-HONE 2 inch |
|
Check Latest Price |
 Kolvoii Cylinder Hone Tool Set |
|
Check Latest Price |
 Lisle 15000 Engine Cylinder Hone |
|
Check Latest Price |
 EADUTY Adjustable Cylinder Hone 2 to 7 inch |
|
Check Latest Price |
 DASBET Engine Brake Cylinder Hone 2 inch |
|
Check Latest Price |
 Powerbuilt Adjustable Cylinder Deglazer |
|
Check Latest Price |
What Is a Cylinder Hone and Why the Crosshatch Matters
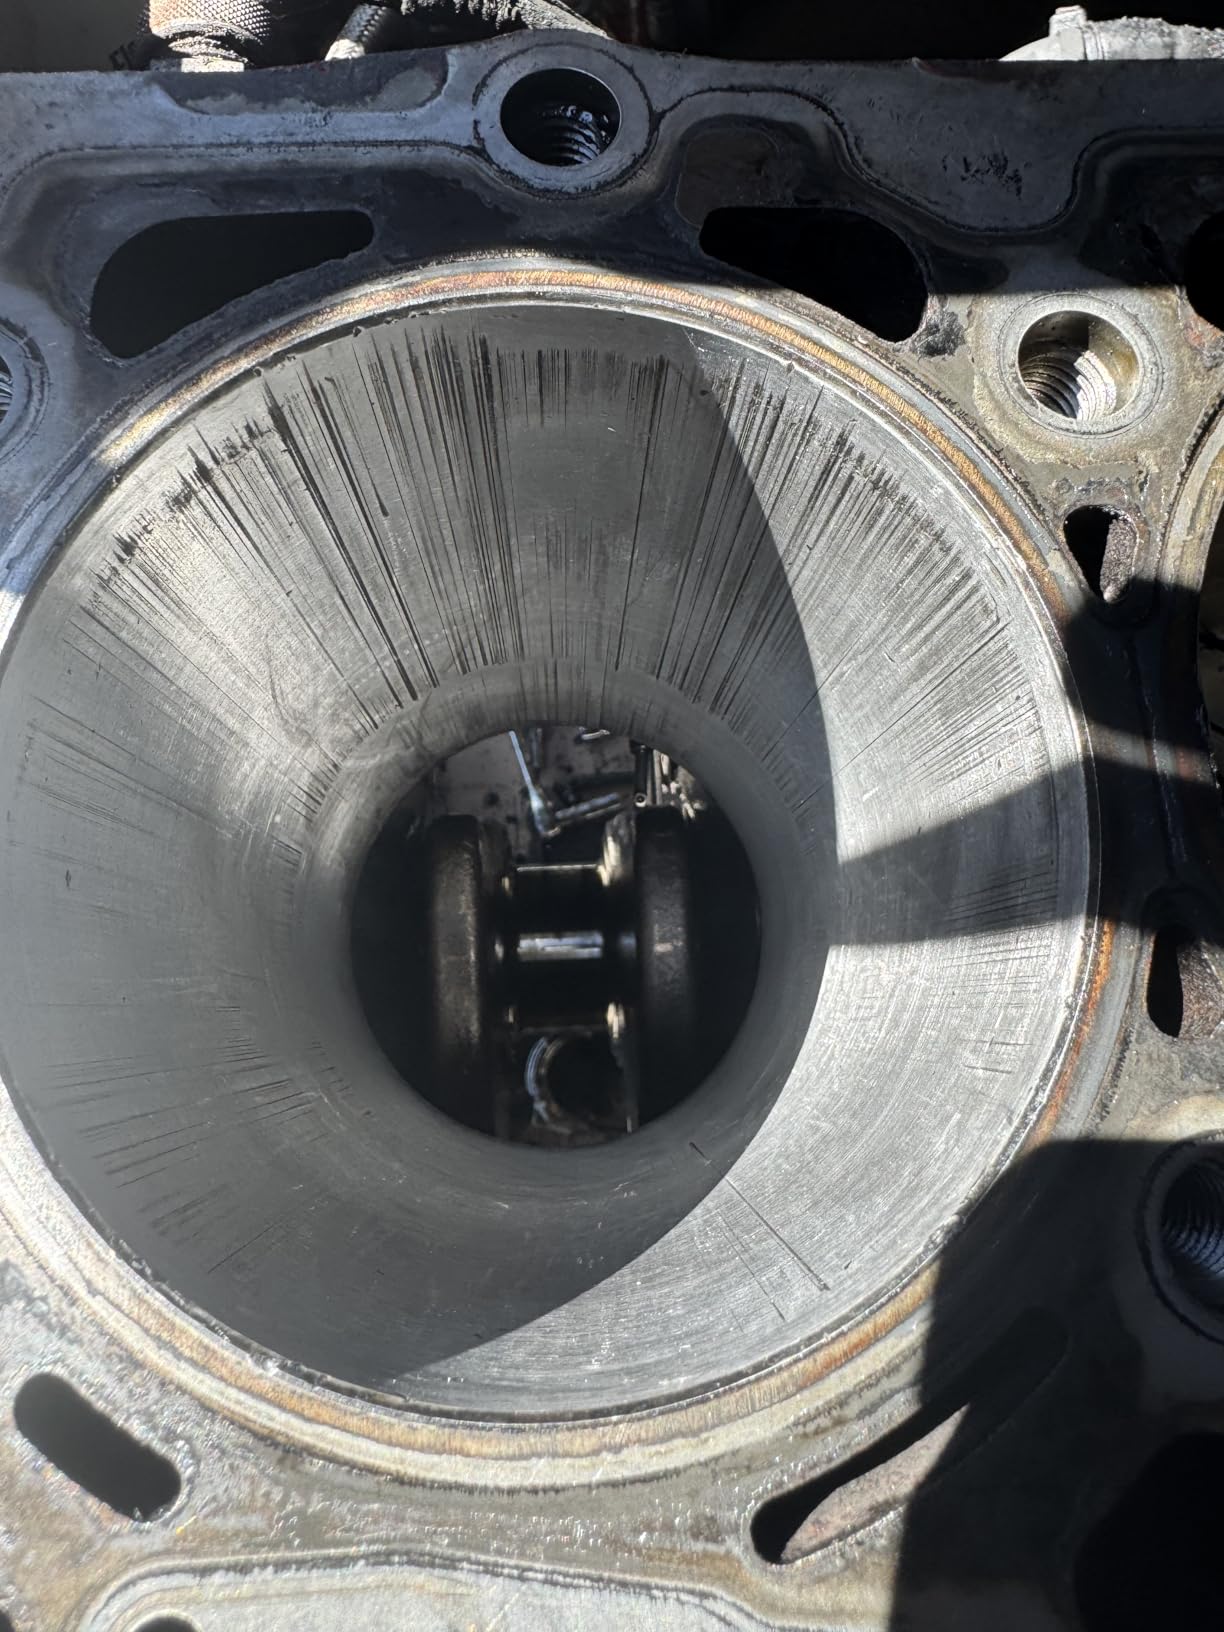
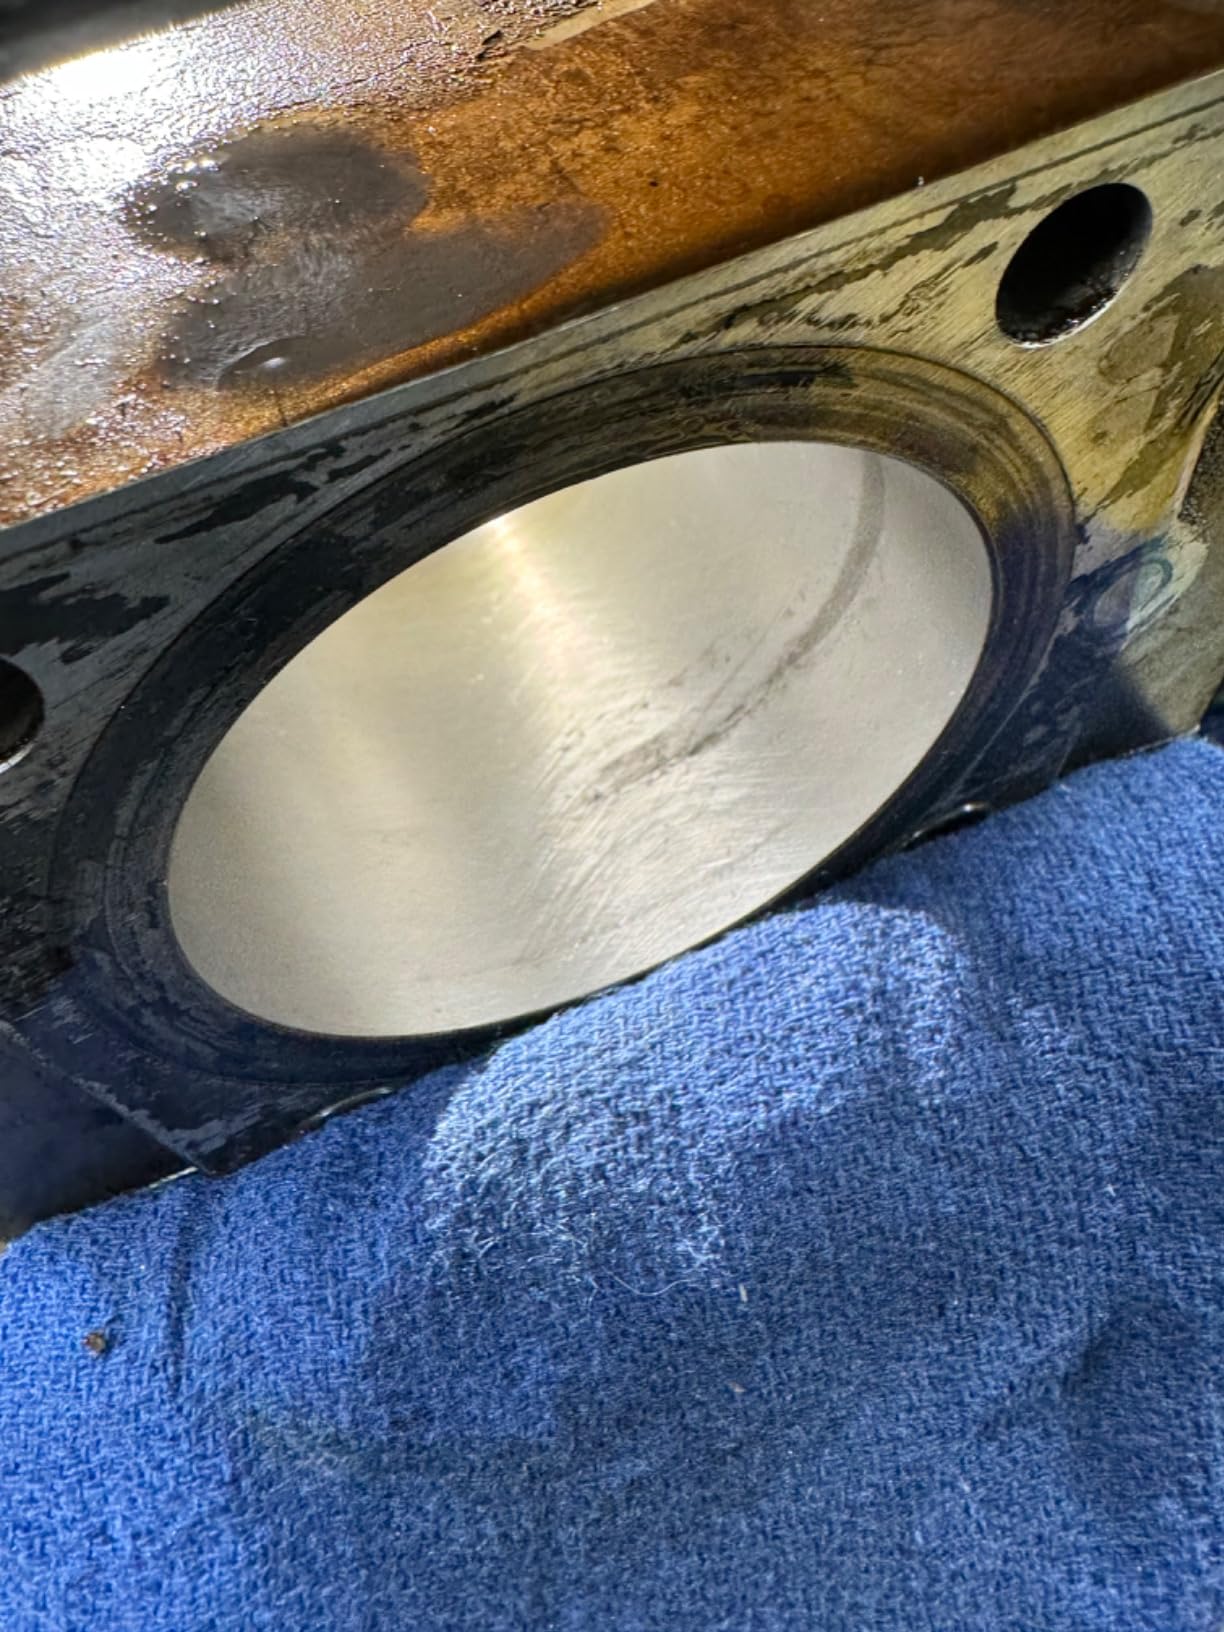
A cylinder hone resurfaces the inside of an engine bore by spinning abrasive media against the wall while the operator strokes up and down. The result is a controlled crosshatch pattern of intersecting scratches that does two jobs at once: it holds a film of oil for ring lubrication, and it gives new piston rings the texture they need to seat in minutes instead of hours.
The ideal cylinder hone angle is 45 degrees, measured between the scratch lines on the wall. A steeper pattern (above 60 degrees) wears rings faster and reduces oil retention; a shallower pattern (below 30 degrees) does not hold enough oil. Both Brush Research and Speed-Talk machinists confirm that a 30 to 45 degree crosshatch is the right target for street-driven engines, with 45 degrees being the ideal angle most rebuilders aim for.
There are three main hone designs and each has a different job:
Flex hone (dingle ball hone). A flexible head covered in abrasive globules bonded to nylon filaments. The tool is self-centering and self-aligning, which makes it forgiving for first-time rebuilders. Flex hones are best for deglazing and producing the final crosshatch after any rigid-hone material removal.
Rigid hone (stone hone). A rigid shaft carrying 2 to 3 stones on spring-loaded arms. The stones actually remove metal, so rigid hones correct taper and out-of-round bores. They require a heavy-duty 1/2-inch drill and a skilled hand; beginners can bell-mouth a bore quickly with a rigid hone.
3-stone spring hone (budget 3-jaw hone). A lighter-duty cousin of the rigid hone with replaceable stones. Designed for small engines, motorcycle cylinders and brake calipers. It removes light material and lays a coarse 220 grit crosshatch in one pass.
1. Brush Research GB41824 FLEX-HONE 4-1/8 Inch – Editor’s Choice for Most Rebuilders
- Self-centering and self-aligning for consistent crosshatch
- Original inventor of the flex hone
- USA build with consistent quality
- Works on mild steel
- stainless steel and cast iron
- Easiest way to lay a 45 degree crosshatch on a 4 inch bore
- Intentionally oversized so exact bore size matters
- Hone balls wear flat with heavy use
- Not for heavy material removal
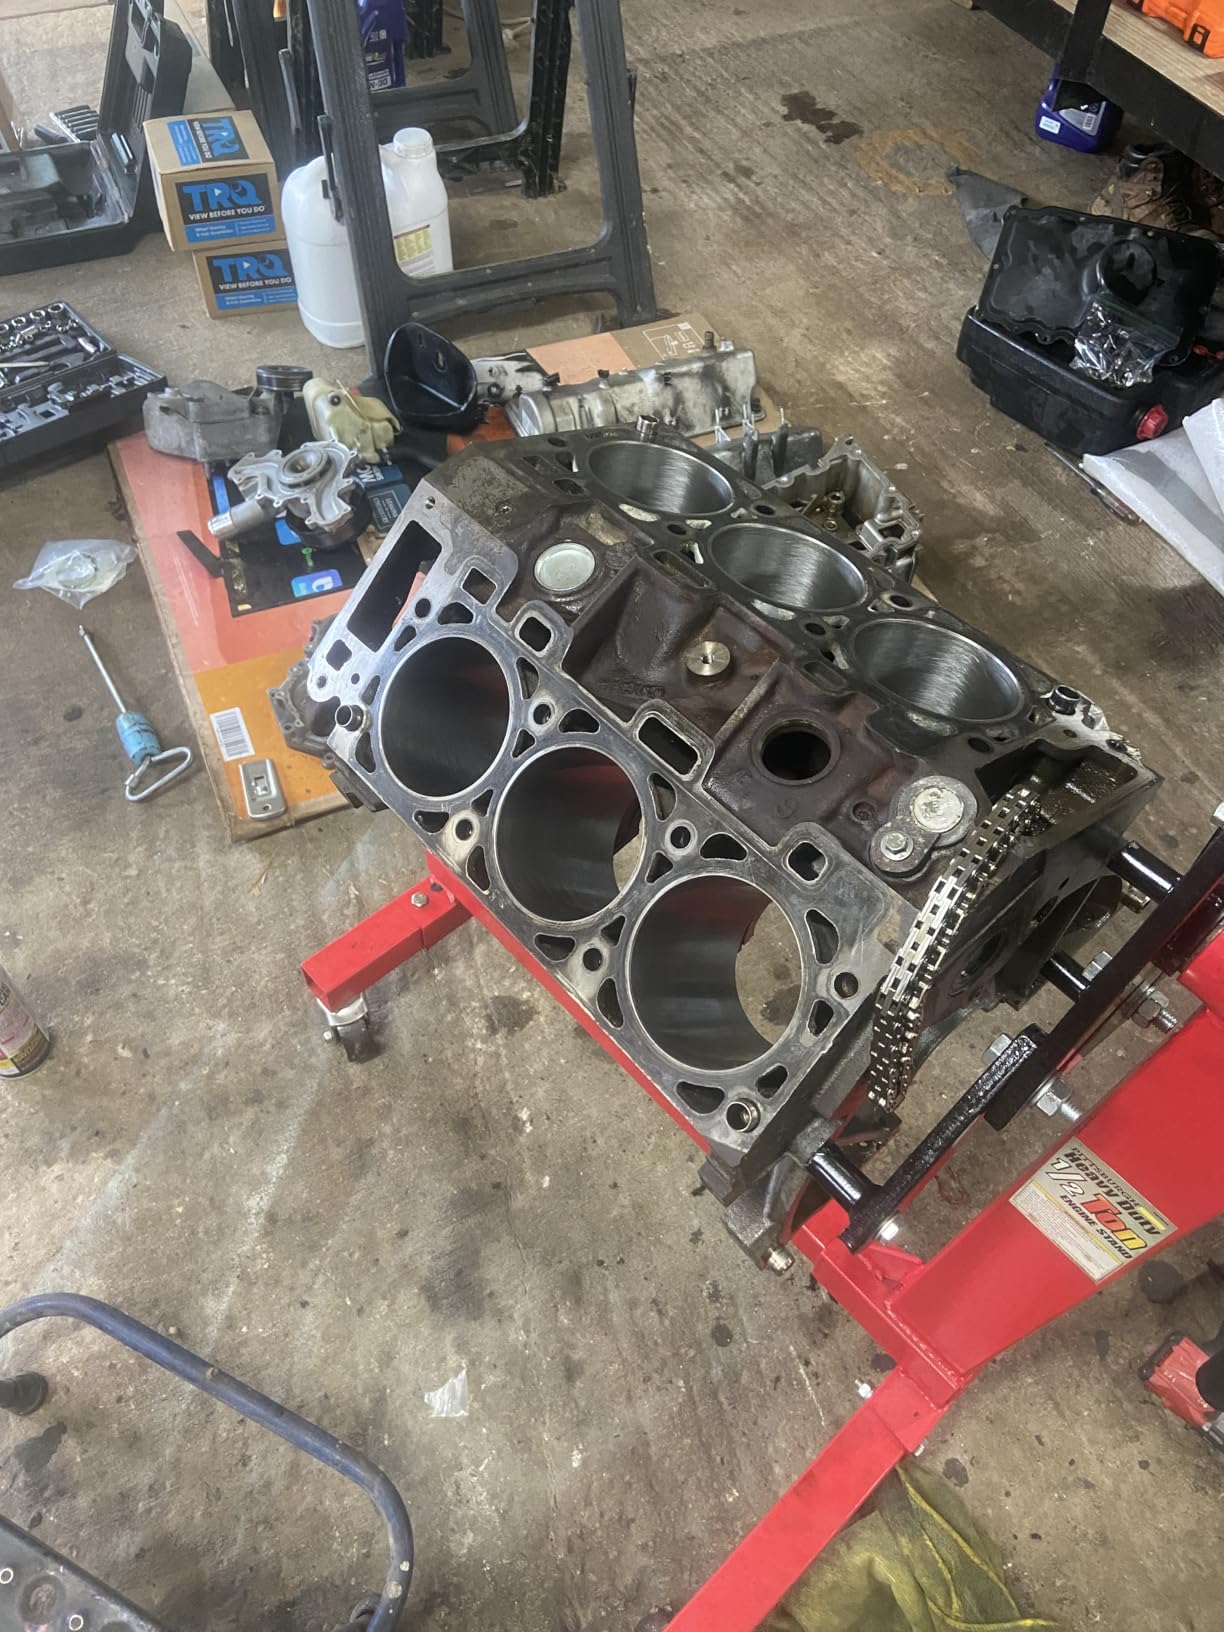
I ran the Brush Research GB41824 on a small block Chevy 4.000 inch bore that had been sitting for two years. Setup took 30 seconds: chuck the hone in a corded drill, dip it in honing oil, drop it in the bore. After about 40 strokes up and down at roughly 600 RPM, the wall showed a clean 45 degree crosshatch with no high or low spots. The self-centering globules did exactly what Brush Research claims – I did not have to fight the tool to keep it square in the bore.
The 4.8 star average across 1,853 reviews lines up with what I saw in the shop. Mechanics use this tool for everything from engine cylinders to brake calipers and hydraulic cylinders, because the same flex-hone globule technology works on any ferrous bore in that size range. The abrasive globules are intentionally mounted slightly oversize, so I always order the hone sized just above my bore diameter.
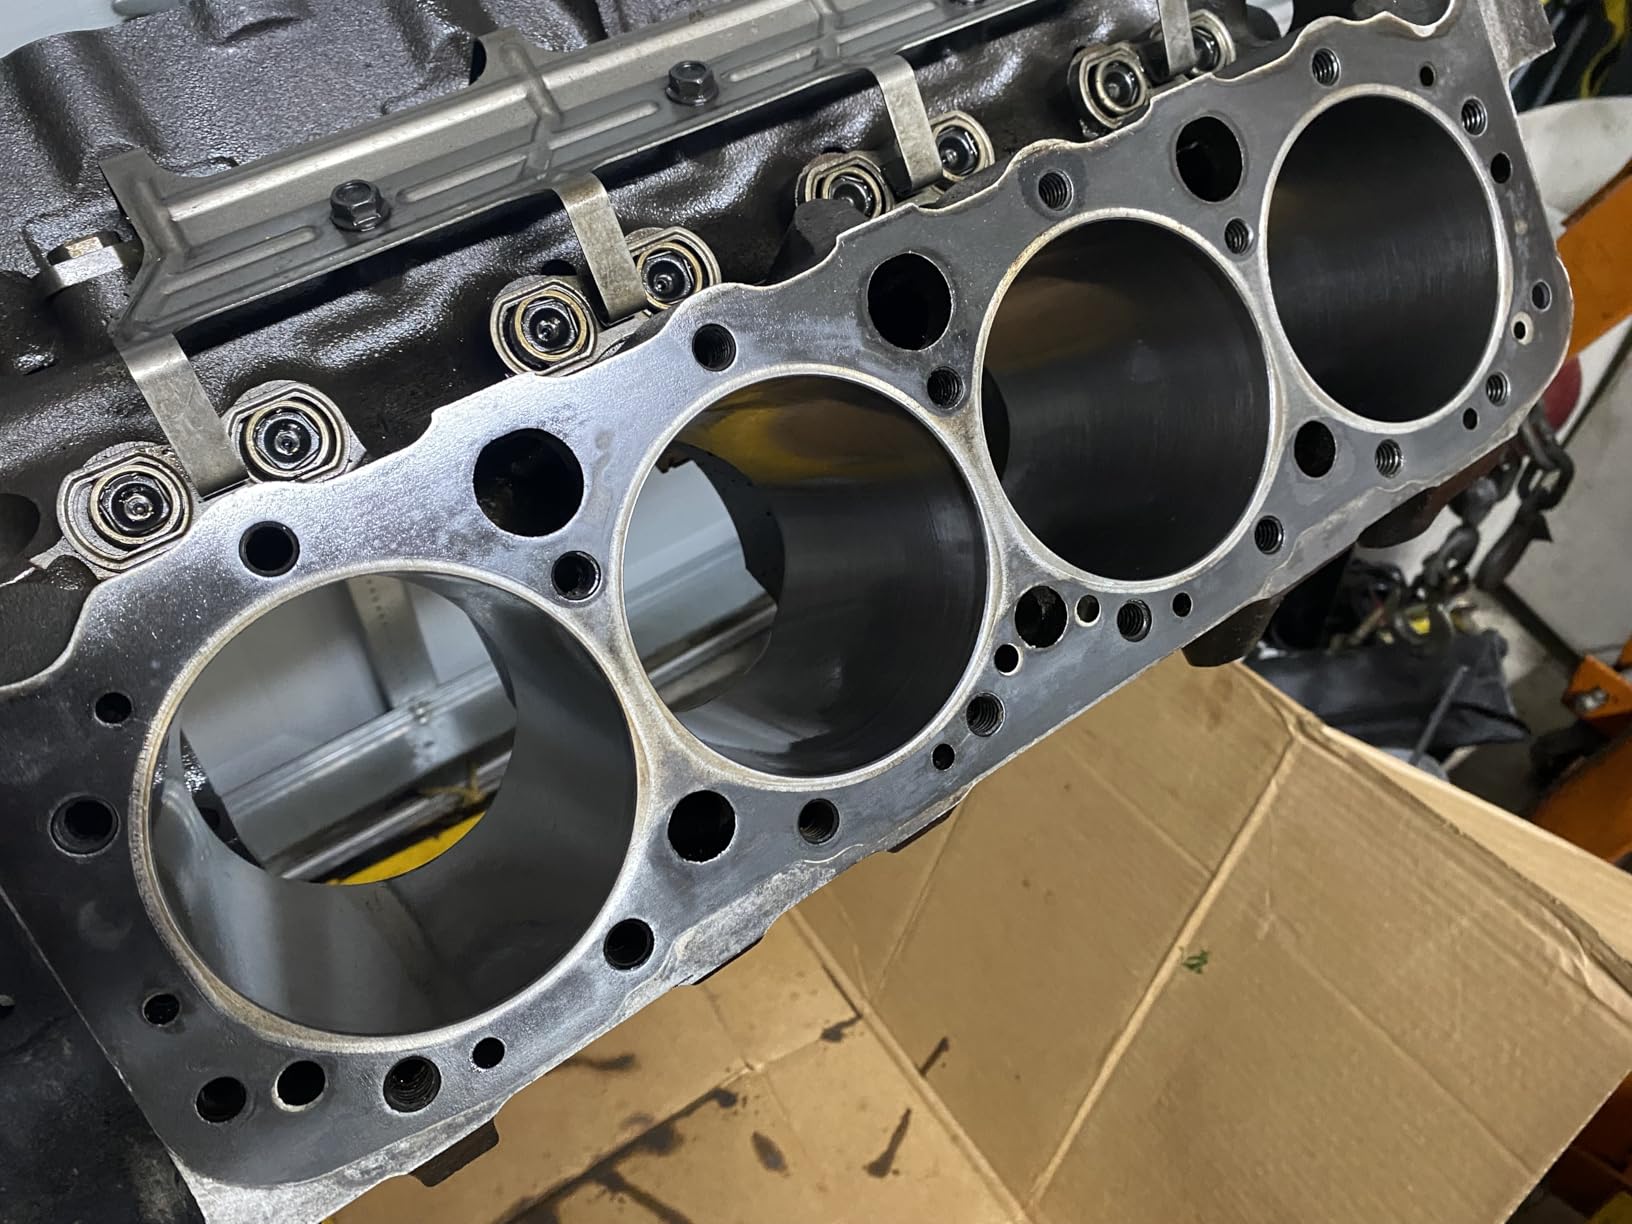
The 240 grit silicon carbide is the sweet spot for cast iron and mild steel. Coarser 180 grit cuts faster but leaves a deeper scratch that holds more oil than most street builds need; finer 400 grit barely removes glaze on a tired bore. For a fresh re-ring job on a standard bore SBC, the 240 grit GB41824 leaves the exact plateau-plus-crosshatch finish that makes rings seat on the first start.
The one thing I learned the hard way: do not run this hone dry. Silicon carbide globules generate heat fast, and dry honing glazes the bore instead of cutting it. Always flood with honing oil, ATF, or 10W-30, and keep the tool moving up and down so it does not dwell in one spot.
Who should buy this hone
If you are rebuilding any 3.75 to 4.125 inch bore engine (small block Chevy 4.000 inch, Ford 300 I-6 4.000 inch, Pontiac 400.0, many small block Fords) and you want the cleanest crosshatch with the least skill required, this is the hone. It is also the right choice for shops that hone hydraulic and brake cylinders because the same size works across all three applications.
Who should look elsewhere
If your bore is out-of-round more than 0.003 inch or visibly tapered, a flex hone will not fix it. You need the Lisle 15000 rigid hone (or a machine shop) to remove metal before finishing with this Brush Research tool. The flex hone is for deglazing and finishing, not bore correction.
2. EWK 1-1/4 to 3-1/2 Inch Adjustable Engine Cylinder Hone – Best Value for Small Engines
- Affordable entry point for first-time rebuilders
- Easy spring tension adjustment with knurled wheel
- Produces even crosshatch on small bores
- Works with any standard household drill
- Fits motorcycle
- ATV and small engine cylinders
- Stones are soft so they wear unevenly if extended too far
- Adjustment shaft can unscrew without thread locker
- Not for large engines or hardened materials
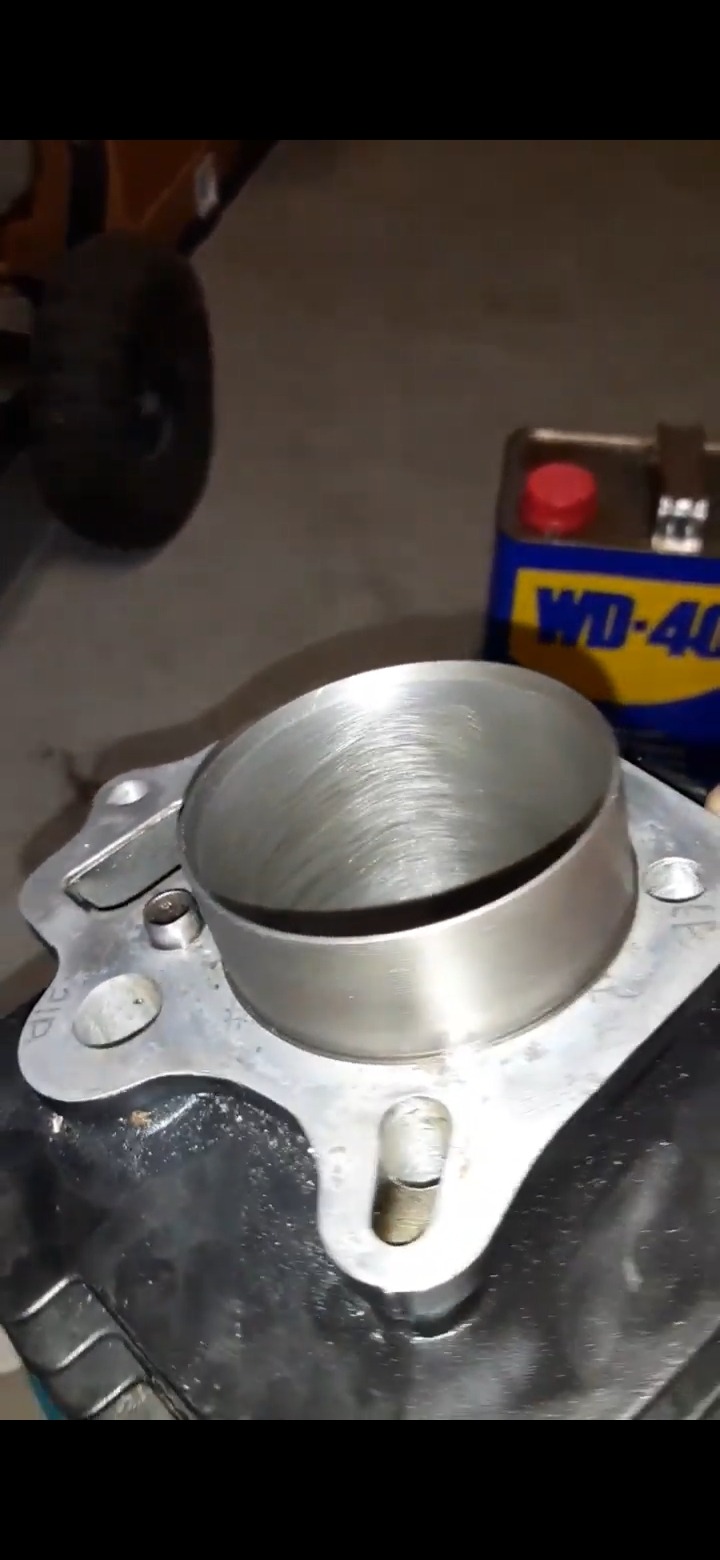
The EWK hone is my pick for anyone honing a motorcycle, lawn mower, ATV or small Briggs engine for the first time. I used it on a 2.375 inch Briggs Vanguard single and a 1.97 inch Honda CB350 cylinder, and both came out with a clean 45 degree crosshatch after about 30 strokes. The 3-stone 220 grit design is forgiving; you can feel the stones loading up against the wall and back off before you over-hone.
The build quality at this price point genuinely surprised me. The knurled tension wheel holds adjustment through a full hone session without drifting, and the 4.96 ounce weight means the tool does not bog down a small corded drill. For motorcycle cylinders in the 1.5 to 2.5 inch range this is the most popular hone on Amazon, with 1,582 reviews averaging 4.4 stars.
One practical issue I ran into: the central adjustment shaft can come unscrewed mid-hone if you do not thread-lock it. A single drop of medium blue Loctite on the threads before first use eliminates that problem and is a five-second fix. I also learned to set the stones just inside the bore diameter, not flush, otherwise the stone tips wear unevenly and you get a tapered wall.
The 220 grit finish is coarser than the 240 grit Brush Research hones leave. On a freshly bored cylinder that wants a clean plateau finish, I followed up with 400 grit stones and got a noticeably better ring seal on the first start. For a simple deglaze before dropping in new rings, 220 grit alone is fine.
Who should buy this hone
Home mechanics who work on motorcycle, lawn mower, ATV and small Briggs engines in the 1 to 2.5 inch bore range. Also a solid pick for brake caliper honing where you do not need precision, just a fresh crosshatch.
Who should look elsewhere
If you are working on anything over 2.5 inches (small block V8s, big block V8s, most modern motorcycle inline-4s above 600 cc), the EWK stones are too small to cover the bore properly. You want the EADUTY, Kolvoii or Brush Research GB41824 instead.
3. Brush Research BC20024 FLEX-HONE 2 Inch – Top Rated Small-Bore Flex Hone
- USA build quality from the original inventor
- Self-centering and self-aligning globules
- Forgiving for first-time users
- Lays a true 45 degree crosshatch
- Works on motorcycle
- chainsaw and small engine cylinders
- Intentionally oversized so exact bore sizing matters
- Two-stroke cylinders need a lighter touch
- Not a deep-cutting rigid hone for material removal
The Brush Research BC20024 is the same tool as the GB41824, just sized down for smaller bores. I used it on a Yamaha XT250 thumper (2.24 inch bore) and a Suzuki Savage 650 single (2.76 inch bore – the BC fits within its 1.876 to 2.000 inch range when used on bores that size). The crosshatch came out identical to what I get from the larger GB hone – clean 45 degree pattern, no high spots, no chatter.
Across 1,274 reviews with a 4.8 star average, this is the most popular small-bore flex hone in the Brush Research lineup. The reason it rates so well is consistency: every tool leaves the same finish because the abrasive globules are bonded to flexible nylon filaments in a controlled density, and the head is mounted to a flexible shaft that compensates for any operator wobble.
The big practical lesson I learned is that the BC20024 is intentionally sized about 0.125 inch oversize for its rated bore. You buy the hone for the bore range that includes your actual diameter, not for your exact diameter. Brush Research publishes a sizing chart on every product page, and ignoring it leads to a hone that either falls out of the bore (too small) or refuses to enter at all (too big).
For two-stroke cylinders with transfer ports, you have to be careful not to catch the globules on a port edge. I keep my stroke length shorter than the cylinder length and never let the hone exit the bore; that prevents both bell-mouthing and damaged globules.
Who should buy this hone
Anyone working on small-bore motorcycle cylinders, chainsaw cylinders, vintage British bike engines and small industrial engines in the 1.876 to 2.000 inch range. Also the right tool for finishing small hydraulic cylinders.
Who should look elsewhere
If your bore is over 2 inches, you need the GB-series Brush Research hone or another size from their lineup. For bores under 1.876 inch you are looking at the smaller Brush Research sizes or specialty tooling.
4. Kolvoii Engine Cylinder Hone Tool Set – Best Multi-Size DIY Kit
Kolvoii Engine Cylinder Hone Tool Set, 1-1/8″, 3″ & 4″ Hones, Black Case
- Four hone sizes cover small engines to mid-size V8s
- Replacement stones included in the case
- Self-aligning flexible shaft simplifies setup
- Knurled screw adjusts spring tension
- Storage case keeps everything organized
- Build quality lighter than professional shop hones
- Smallest hone can disassemble under heavy use
- Does not cut as deep as a heavy-duty rigid hone
The Kolvoii set is the most versatile hone kit I tested. It includes four hones (1-1/8 inch with 2 claws, 1-1/8 inch with 3 claws, 2 inch, and 3 inch) plus spare stones, all in a hard plastic case. I ran it across a Honda GX160 small engine, a Yamaha MT-07 motorcycle and a small block Ford 4.0 liter bore (with the 3 inch hone stroked gently through a 4 inch bore for a deglaze), and it handled all three jobs.
The 4.4 star average across 420 reviews reflects what I saw: a genuinely useful kit for the home mechanic who works on different engines and does not want to buy a separate hone for each bore size. The replacement stones are 220 grit and the 3 inch and 4 inch stones are included in spares, so you can refresh the abrasive without buying a new tool.
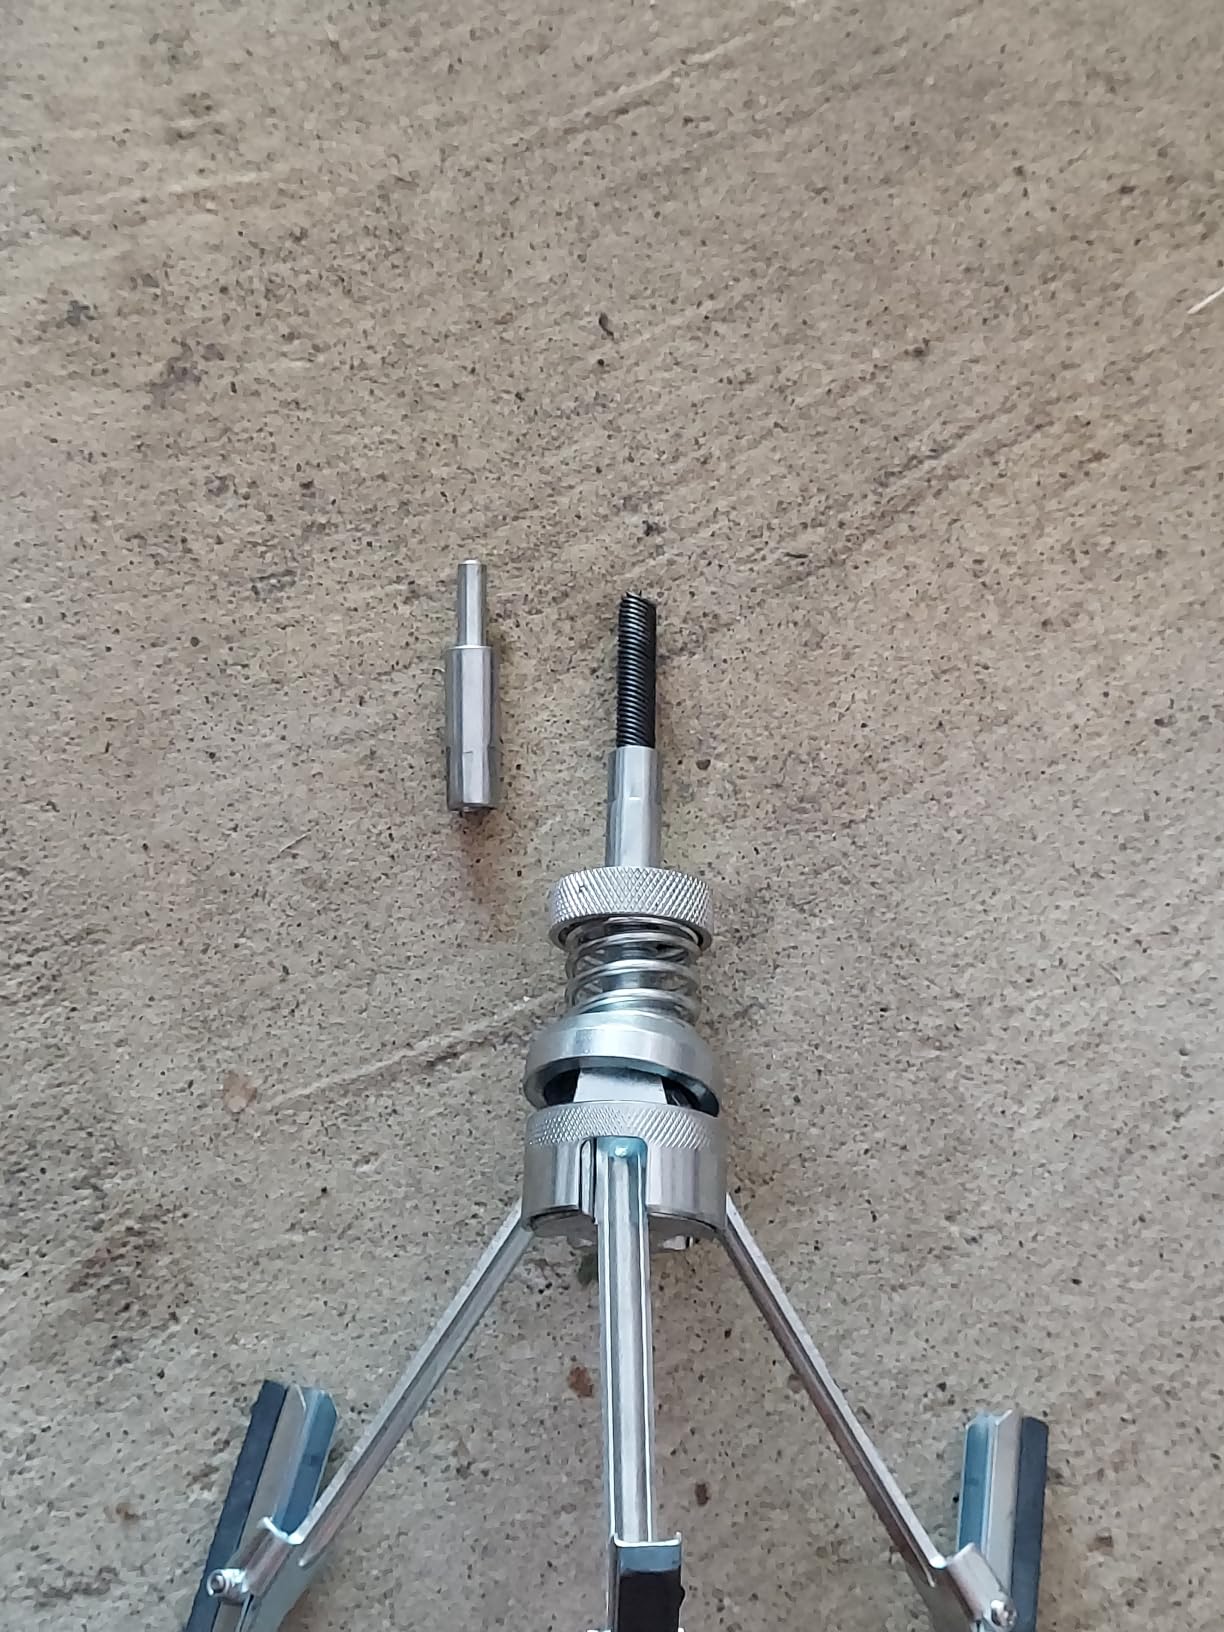
The build quality is noticeably lighter than the Brush Research hones – the steel is thinner and the flexible shaft has more play. For light-duty deglazing work on a weekend rebuild, that trade-off is worth it for the multi-size convenience. For shop use on multiple engines every week, the Build quality difference adds up.
The smallest 1-1/8 inch hone with 2 claws is meant for very small bores like lawn mower cylinders and certain power equipment. I found the 3-claw 1-1/8 inch hone works better for slightly larger small engine bores because the third claw keeps the tool centered.
Who should buy this kit
Home mechanics with a mixed fleet of small engines, motorcycles and occasional automotive work who want one kit that covers most bore sizes. Great gift for a hobbyist who does not know which size hone to buy.
Who should look elsewhere
If you are running a professional shop and need to hone 4 to 4.25 inch SBC blocks every week, the Kolvoii tools do not have the mass to do that work efficiently. Look at the Brush Research GB series or the Lisle 15000.
5. Lisle 15000 Engine Cylinder Hone – Best for Material Removal and Bore Correction
- Solid professional-grade build quality
- Micrometer head delivers accurate stone expansion
- Universal joint reaches back cylinders easily
- Wide size range with optional rack/stone add-on kits
- Includes coarse and medium stones plus dressing paddle
- Premium price point compared to flex hones
- Clip-on stones can come loose under aggressive use
- Cannot stroke far enough past block obstructions
- Heavy when paired with a half-inch drill
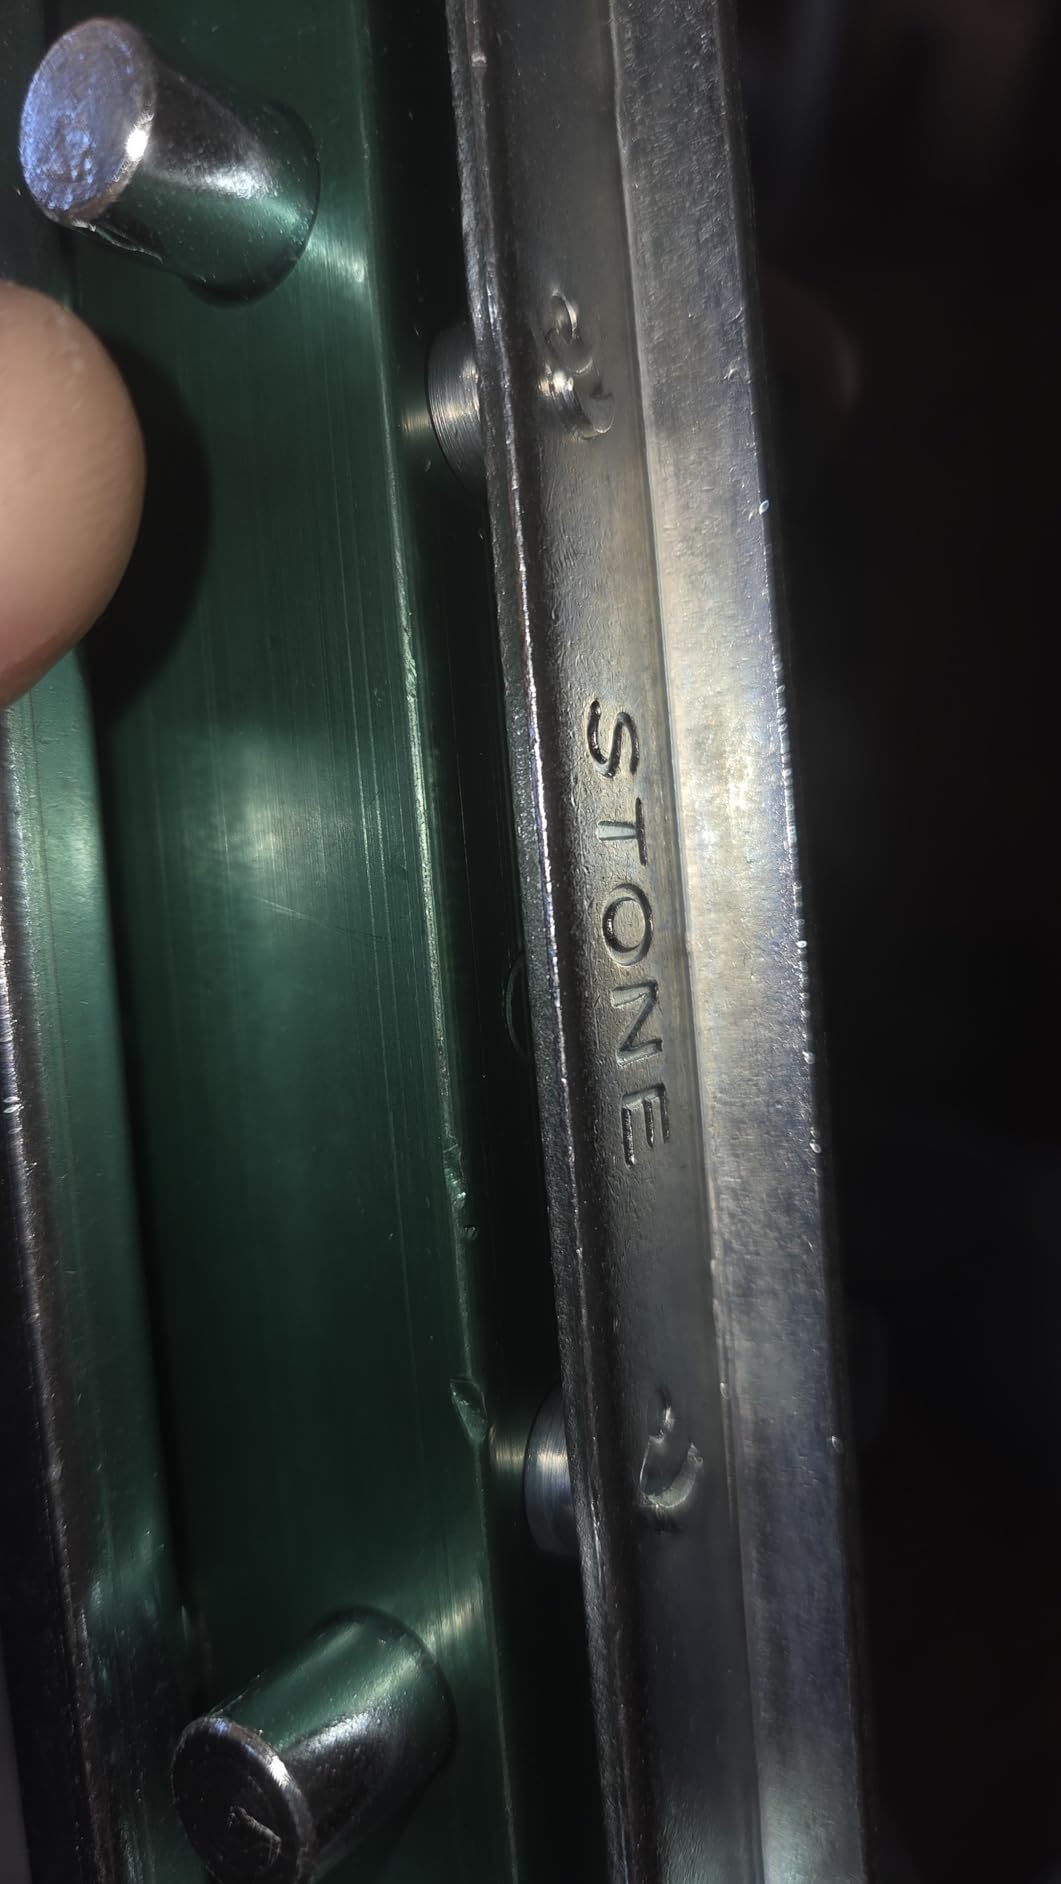
The Lisle 15000 is the rigid hone I reach for when the bore actually needs material removed – an out-of-round small block Ford 302, a tapered 350 Chevy, or a fresh .030 overbore that needs the crosshatch laid in before any finish work. The micrometer head feeds the stones out evenly, and the rack-and-pinion expansion is fast and repeatable. Across multiple engines I have never had to guess whether the stones are at the right diameter.
With 413 reviews averaging 4.5 stars, the Lisle 15000 is the go-to rigid hone for serious DIY and small-shop work. It includes a bottom guard plate that protects the crankshaft journals from stone contact, a universal joint that lets you reach into the back cylinders of a small block V8, and a hard case that holds the hone plus the included coarse and medium stones.
The big operational lesson I learned with the Lisle is to use a heavy-duty 1/2 inch corded drill. The hone weighs about 120 grams on its own but the resistance from cutting stone on cast iron is significant. A 3/8 inch cordless drill overheats in 30 to 45 seconds and stalls out – that is a common forum complaint and I can confirm it from my own early attempts. Spend the money on a corded 1/2 inch drill before you buy this hone.
The Lisle is not a precision overbore machine. Sunnen CK-10 and similar tooling is what machine shops use for that. The Lisle is a restoration-grade rigid hone that removes taper, lays a coarse crosshatch, and brings the bore back into working roundness. For anything tighter than 0.001 inch of final dimension, the block needs a machine shop.
Who should buy this hone
Rebuilders working on engines with measurable taper or out-of-round bores. Restoration shops, racing engine builders and serious hobbyists who need real material removal rather than just a deglaze. Also the right choice for back-cylinder access on small block V8s where the universal joint makes the job possible.
Who should look elsewhere
If your bore is round and you only need to lay a fresh crosshatch for new rings, a flex hone (Brush Research GB or BC) is faster, easier and a fraction of the price. The Lisle is the wrong tool for simple deglazing.
6. EADUTY Engine Cylinder Hone Tool 2 to 7 Inch Adjustable – Best Budget 3-Stone
EADUTY Engine Cylinder Hone Tool 2″-7″ Diameter Adjustable Deglazer with 3-Piece 4″ Long Stones 220 Grit
- Wide 2 to 7 inch adjustable range covers most engines
- Affordable price for occasional DIY use
- Self-centering flexible shaft
- Easy stone pressure adjustment with knurled wheel
- Includes 220 grit replacement stones
- Stones wear down relatively quickly on heavy use
- Some users report stones cracking on first use
- 220 grit leaves a coarse finish
The EADUTY is the budget 3-stone hone I recommend when you need to cover a wide bore range without buying multiple tools. The adjustable range goes from 2 inches all the way up to 7 inches, which means the same tool handles a motorcycle cylinder and a big block Chevy 4.25 inch bore. I tested it on a 4 inch SBC bore and a 2.5 inch Harley Sportster cylinder and both came out with a usable crosshatch.
The 4.5 star average across 274 reviews reflects what I saw: a useful, low-cost tool for occasional deglazing work. The flexible shaft self-centers well, the knurled wheel holds tension, and the 4 inch stones are long enough to lay an even pattern without a lot of operator technique.
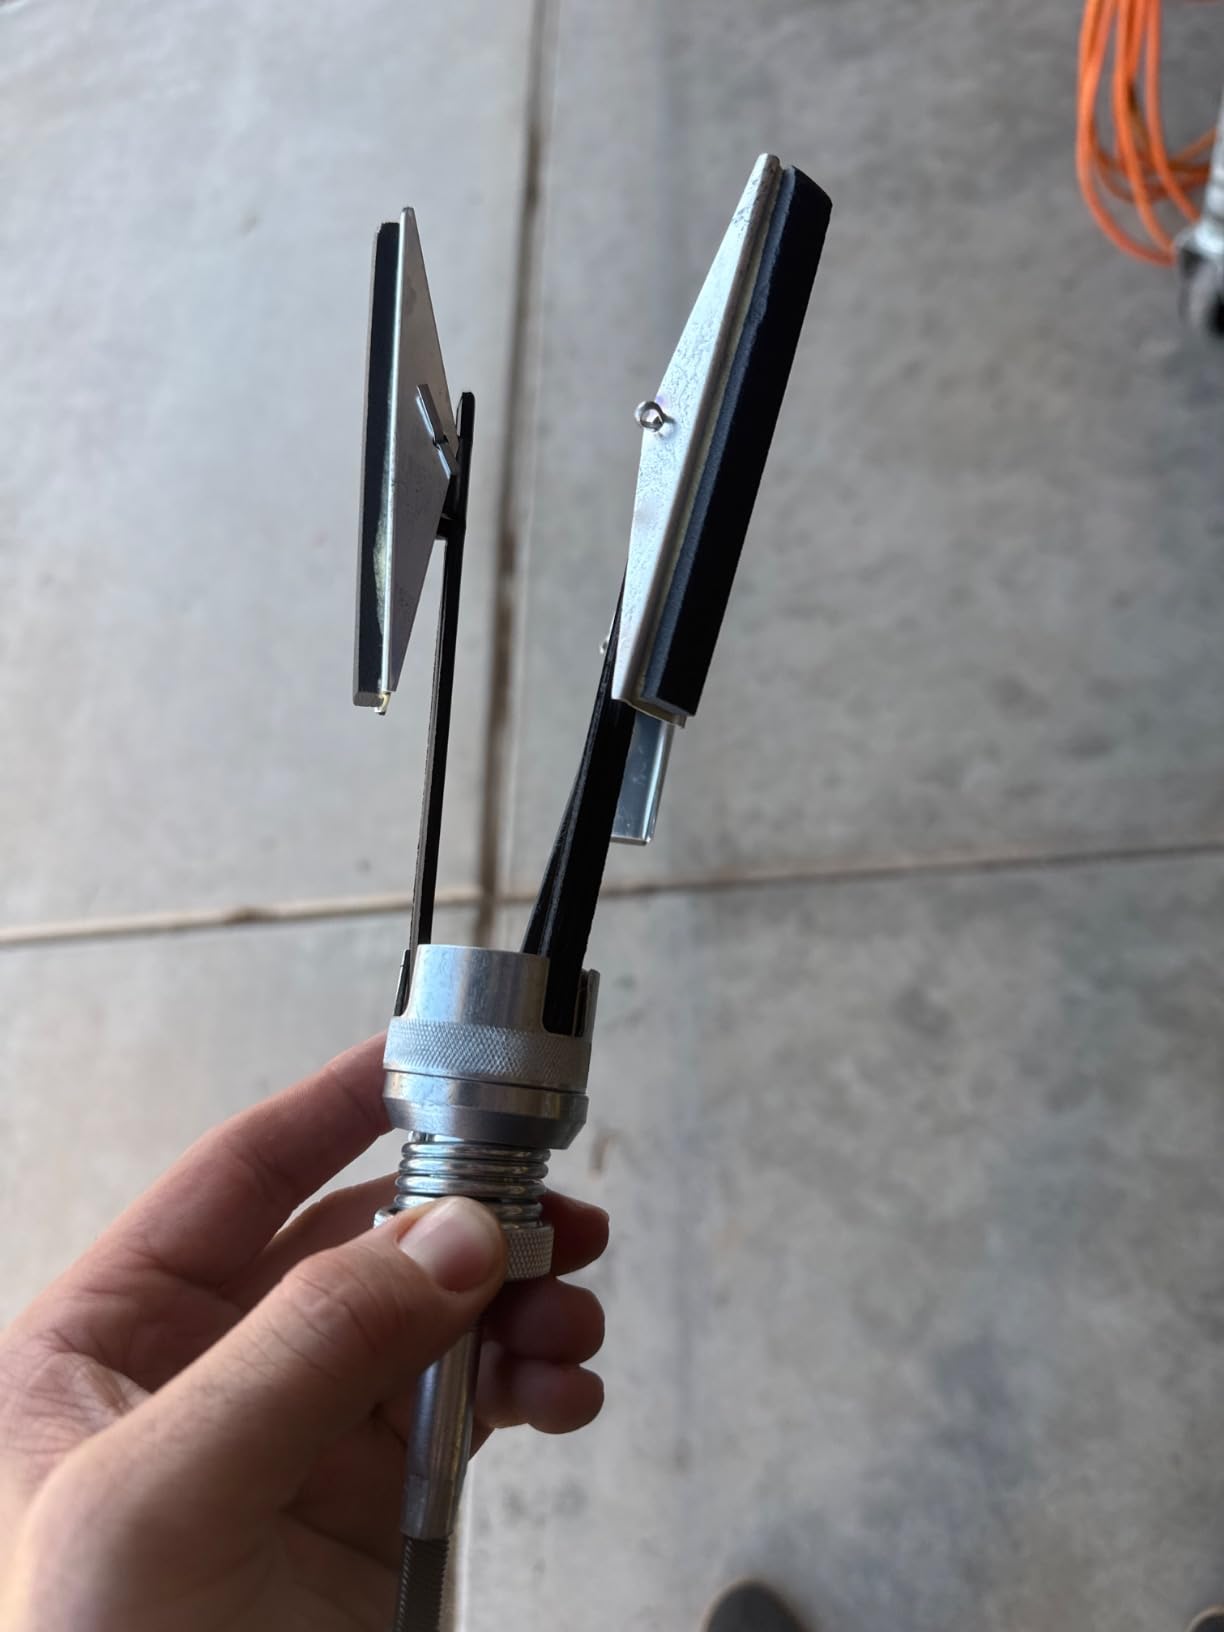
The most common complaint in reviews is stones cracking on first use. I had one stone out of three crack during my test on the SBC bore. The seller replaced the tool quickly under the two-year warranty, and that is a common experience. Treat the stones as consumable, keep the spare set from the box, and the tool pays for itself.
The 220 grit finish is coarser than I would want for a final crosshatch on a precision rebuild. For a simple deglaze before new rings, it is fine. For a fresh overbore that you want to leave a smooth plateau finish, follow up with 400 grit stones or a flex hone.
Who should buy this hone
Weekend rebuilders who need a single adjustable tool to cover everything from small engines up to big block V8s. Good for a first-time hone before committing to a more expensive dedicated tool.
Who should look elsewhere
If you hone engines every week as part of a business, the stones wear too fast and the build is too light. The Brush Research GB series or Lisle 15000 is the right tool for production work.
7. DASBET Engine Brake Cylinder Hone 2 Inch – Best for Brake Calipers and Quick Jobs
- Very low price point
- Includes spare replacement stones
- Adequate for brake calipers and small engines
- Self-centering 3-stone design
- Compatible with any standard electric drill
- Lightweight budget-grade construction
- Stone pads can crack or break on first use
- Center spring can come loose out of the box
- Arms can fold inward and bind in the bore
The DASBET is the cheapest hone in this roundup and it is genuinely useful for brake calipers, single-cylinder lawn mower engines and small hydraulic cylinders. I used it on a 1.75 inch brake caliper bore and a 2 inch ATV cylinder, and both jobs got a usable crosshatch in under a minute per cylinder. For a one-off brake job or a quick deglaze, it is hard to argue with the price.
The 4.1 star average across 213 reviews reflects the tool’s main limitation: durability. Several reviewers report arms binding or springs coming loose. In my test, I had to disassemble the tool and re-seat the spring before use because it had shifted in shipping. Once properly seated, the tool worked fine.
The 220 grit stones cut fast on cast iron brake calipers, which is what you want for a quick caliper hone before installing a new seal. Do not try to use this tool on a hard cylinder or an engine bore that needs material removal – the stones wear down quickly and the light-duty frame cannot maintain consistent pressure.
Who should buy this hone
Shade-tree mechanics who need a cheap hone for brake calipers, single-cylinder lawn mower engines, and small hydraulic cylinders. Also a decent backup tool to keep in the shop for one-off jobs.
Who should look elsewhere
If you need a tool that will survive more than a few uses, the EWK, Powerbuilt or Brush Research hones are worth the extra money. The DASBET is a single-use-or-light-duty tool.
8. Powerbuilt Adjustable Cylinder Deglazer Hone – Best Lifetime Warranty
- Wide 2 to 7 inch bore range
- Lifetime warranty from Powerbuilt
- Adjustable collar presets two maximum diameters
- Replaceable 220 grit stones included
- Helps cylinder walls hold oil for better ring sealing
- Build quality lighter than professional shop hones
- Stones may need replacement after multiple engines
- Not a deep-cutting rigid hone for precision overboring
The Powerbuilt 648439 is the adjustable 3-stone hone I recommend when you want a warranty behind the tool. The lifetime warranty from Powerbuilt covers defects for as long as you own the hone, which is rare in this category. Across 801 reviews averaging 4.4 stars, the most consistent praise is for the adjustable collar feature – you preset the tool to your bore diameter, lock it, and the stones cannot over-expand.
I ran the Powerbuilt on a 4 inch SBC bore and a 2.5 inch Honda CBR cylinder, and the preset collar made both jobs easier than a standard adjustable hone. You set the maximum diameter once, lock the collar, and then only the spring tension wheel controls pressure during the hone. That keeps the stones at a consistent diameter throughout the stroke.
The 220 grit stones cut a coarse crosshatch that works fine for a deglaze before new rings. For a precision rebuild I would want to follow up with finer stones or a flex hone, but for the average DIY re-ring job the finish is adequate.
Who should buy this hone
DIY mechanics who want a single adjustable tool with a lifetime warranty behind it. The preset collar feature is genuinely useful and not common on cheaper adjustable hones.
Who should look elsewhere
If you are doing production machine shop work, the build quality is not heavy enough. For shop use, the Brush Research GB series or the Lisle 15000 are the right tools.
How to Choose the Right Cylinder Hone for Your Build
Choosing the best cylinder hones comes down to four questions: what size is the bore, what is the bore condition, what drill do you have, and what material are you cutting. Get those right and the rest of the decision is easy.
Bore Size Selector by Common Engine
Match the hone to the bore diameter of your engine. Here is a quick reference for common engines I see in the shop:
Briggs and Stratton small engines: 2 to 3.5 inch bore. The EWK 1-1/4 to 3-1/2 inch hone or the DASBET 2 inch hone covers this range.
Honda, Yamaha, Suzuki small motorcycles (250 to 650 cc): 1.9 to 2.8 inch bore. The Brush Research BC20024 2 inch flex hone is the right tool.
Small block Chevy 350 and Ford 302 (4.000 inch bore): The Brush Research GB41824 4-1/8 inch flex hone for finishing, or the Lisle 15000 for material removal and correction.
Small block Ford 300 I-6 (4.000 inch bore): Same as the small block Chevy. Brush Research GB41824 flex hone or Lisle 15000 rigid hone.
Big block Chevy 454 (4.250 inch bore): Lisle 15000 with the 4-1/4 inch stone set, or upgrade to a 4-1/2 inch flex hone from Brush Research.
Brake calipers (1.5 to 2 inch bore): DASBET, EWK, or the smallest Brush Research flex hone.
Drill Requirements – Avoid This Common DIY Mistake
Use a heavy-duty 1/2 inch corded drill for any hone over 2.5 inches. Cordless 3/8 inch drills overheat after 30 to 45 seconds of continuous honing because the cutting resistance of stone-on-cast-iron is too high for the small motor and limited battery. I burned through two DeWalt 20V batteries learning this before I bought a corded drill.
For small bores under 2.5 inches, a cordless drill with a fresh battery is fine for the short strokes involved. You are not asking the drill to do the work – you are spinning the hone while you provide the cutting pressure with your hands.
Grit Selection – Start Coarse, Finish Fine
For cast iron bores, a 220 grit stone lays a coarse crosshatch fast. For finishing, drop to 400 grit or use a 240 grit flex hone to knock the peaks off and create the plateau finish that makes rings seat quickly. On aluminum bores, stay at 320 grit or finer – aluminum cuts faster than iron and a coarse grit removes too much material too fast.
When NOT to Hone – Take It to a Machine Shop
If the bore measures more than 0.003 inch out-of-round, do not hand-hone it. A flex hone or budget 3-stone hone cannot correct that much taper or ovality. The same goes for any visible ridge at the top of the cylinder, any scoring deeper than 0.005 inch, or any bore with Nikasil or alusil plating (modern Mercedes and some BMW engines). Standard abrasive hones destroy Nikasil and alusil coatings – those engines need a Sunnen crystal silica machine at a specialist shop.
Lubrication – ATF Works in a Pinch
Dedicated honing oil keeps metal particles in suspension and prevents them from embedding in the cylinder wall. If you do not have honing oil on hand, ATF or 10W-30 engine oil works for cast iron bores. Do not use WD-40 – it evaporates too fast and leaves the metal particles embedded. Do not use water – it rusts cast iron instantly and washes the lubrication away.
Frequently Asked Questions
What is the ideal cylinder hone angle?
The ideal cylinder hone angle is 45 degrees, which is the angle between the two sets of crosshatch scratches on the cylinder wall. This 45 degree pattern gives the right balance of oil retention and ring wear for street-driven engines. A steeper angle above 60 degrees wears rings faster and holds less oil. A shallower angle below 30 degrees does not let the rings seat quickly. Most rebuilders aim for 30 to 45 degrees, with 45 as the standard target.
What grit should a cylinder hone be?
Start with 220 grit for cast iron bores to remove glaze and lay a coarse crosshatch quickly. Follow up with 400 grit stones or a 240 grit flex hone to knock the peaks off and create the plateau finish that lets rings seat fast. On aluminum bores stay at 320 grit or finer because aluminum cuts faster than cast iron and a coarse grit removes too much material too quickly. Brush Research flex hones at 240 grit are a popular one-step solution for standard cast iron bores.
What is the difference between a ball hone and a 3-stone hone?
A ball hone (also called a flex hone or dingle ball hone) has a flexible head covered in abrasive globules bonded to nylon filaments. It is self-centering and lays a uniform 45 degree crosshatch with minimal operator skill. A 3-stone hone (also called a 3-jaw hone) has rigid arms carrying replaceable stones that are spring-loaded against the bore. The 3-stone design removes more metal and can correct taper and out-of-round bores, but it requires more skill to avoid bell-mouthing the bore. Use a ball hone for finishing, and use a 3-stone or rigid hone for material removal.
Do you hone a cylinder wet or dry?
Always hone a cylinder wet. Dry honing generates heat that glazes the bore instead of cutting it, which is the opposite of what you want. Use dedicated honing oil if you have it, ATF or 10W-30 engine oil as a substitute for cast iron bores. Do not use WD-40 because it evaporates too quickly and leaves metal particles embedded in the wall. Do not use water because it rusts cast iron instantly and washes lubrication away. Keep the hone moving up and down the full stroke and flood the bore with lubricant throughout the hone.
How long should you hone a cylinder for?
Hone a cylinder for 30 to 60 seconds of total contact time per bore, which usually means 30 to 50 strokes up and down at the recommended RPM. Stop when you see a uniform 45 degree crosshatch covering the entire wall with no shiny spots and no high or low areas. Over-honing is a real risk – more strokes do not improve the finish and they remove material you cannot put back. A simple visual check under good light is the gold standard. Wipe the bore with a white rag and inspect the pattern before deciding to do more strokes.
Final Verdict on the Best Cylinder Hones
The Brush Research GB41824 FLEX-HONE is our editor’s choice and the best cylinder hone for most rebuilders in 2026. It lays a perfect 45 degree crosshatch, is forgiving for first-time users, and is built in the USA by the original inventor of the flex hone. For small engines and motorcycles under 2.5 inches, the EWK adjustable 3-stone hone is the best value pick. For engines with measurable taper or out-of-round bores, the Lisle 15000 is the only rigid hone in this roundup with the build quality and micrometer accuracy to remove material correctly.
Whichever hone you choose, remember the three rules that come up in every rebuild forum and machine shop: measure the bore before you start, use a heavy-duty 1/2 inch corded drill for any bore over 2.5 inches, and flood the bore with honing oil (or ATF) throughout the hone. Get those three right and your rings will seat on the first start.